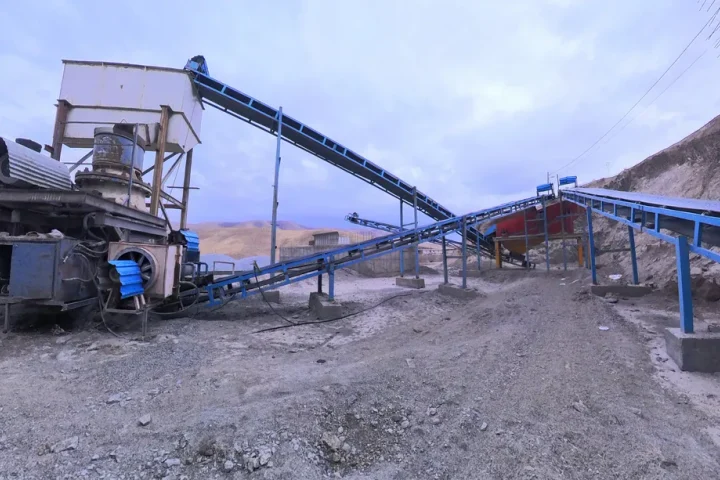
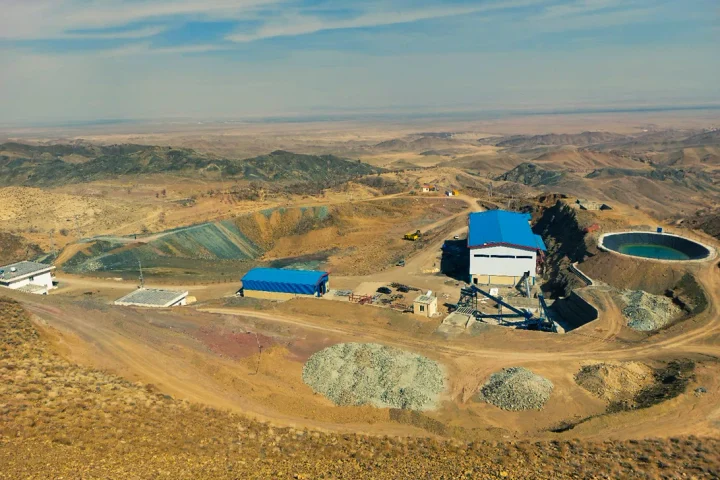
Define what plant optimisation should improve
Higher recovery, stable product quality, lower specific energy and fewer unplanned stops are different objectives. They may support each other, but they can also involve trade-offs. The first step is to agree which outcomes matter and how they will be measured.
A Zarfaravar optimisation review begins with the operating context: ore changes, throughput, product requirements, equipment condition and current control practices. A single poor production day is not a reliable baseline for an improvement claim.
- Recovery and product specification
- Throughput and operating stability
- Specific energy, water and reagent use
- Availability and unplanned interruption
Use representative sampling and a balanced circuit
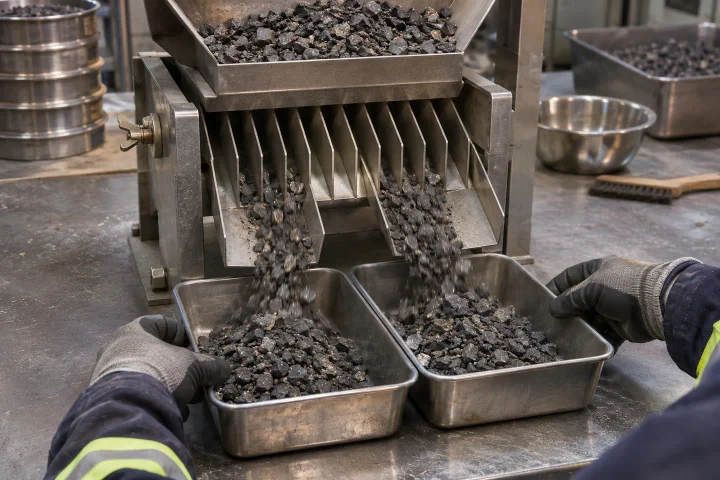
Circuit sampling needs a defined operating state, suitable sample points and enough information to relate the streams. Feed and product assays taken at unrelated times may create an apparent loss that is actually a sampling or inventory effect.
A reconciled mass balance helps identify where the measurements agree and where uncertainty remains. Laboratory results, flow measurements and plant history should be reviewed together before diagnosing a unit as the source of the problem.
Follow losses through grinding and separation
A separation problem can originate upstream. Changes in liberation, particle-size distribution, slurry conditions or circulating load may influence recovery and concentrate quality. Adjusting a downstream unit without examining these inputs can hide the cause temporarily.
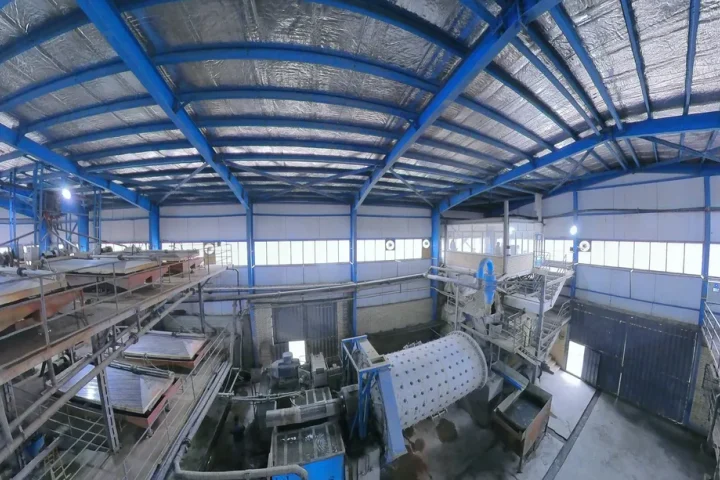
Zarfaravar considers the connected circuit rather than isolated equipment settings. Targeted tests can distinguish material-related limits from control, mechanical or operating issues and help select the next useful trial.
- Feed variability and liberation
- Classification and circulating loads
- Separation conditions and product quality
- Dewatering and return-water effects
Compare actions before buying new equipment
Possible actions range from measurement corrections and operating procedures to control changes, maintenance work or capital modifications. Each option should be compared for expected effect, uncertainty, implementation effort and shutdown requirements.
A prioritised register helps separate quick, reversible trials from changes that need additional engineering. The review should not assume that a new machine is the solution before the constraint has been demonstrated.
Verify improvement without confusing the variables
Before-and-after results should be compared under sufficiently similar feed and operating conditions. Changes in ore hardness, grade, production rate or measurement method can otherwise be mistaken for the effect of the intervention.
Trial conditions, success criteria and the monitoring period should be agreed in advance. Zarfaravar can structure this measurement plan so that the client sees both the observed change and the limits of the evidence; a recovery or energy saving should not be guaranteed without plant-specific support.
Separate improved recovery from higher feed rate
The Tuzlar gold leaching expansion is described as targeting capacity, extraction efficiency and equipment performance. Those objectives need separate measures: additional feed is useful only if losses in recovery or quality do not cancel out the benefit.
Prepare feed and product records, stream assays, reagent consumption and downtime information. The study programme then establishes baseline indicators and how the effect of changes will be assessed.